Flagship High-Density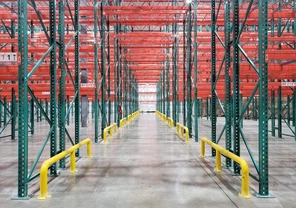
Heavy-Duty Motorized Mobile Racking System
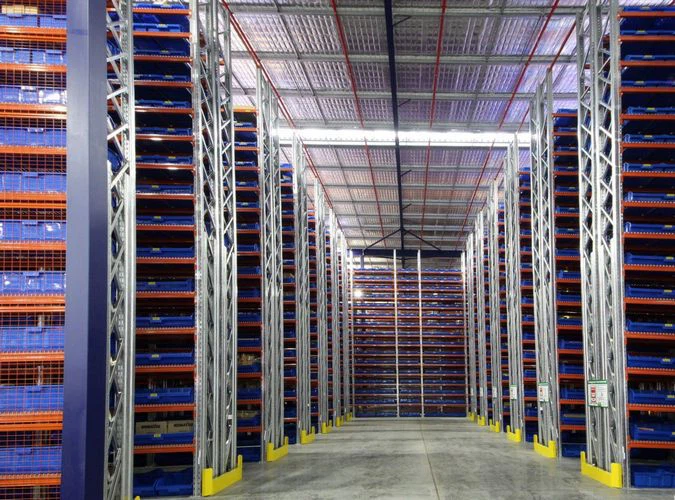
Mounted on electric mobile bases with floor-guided rails. Provides 100% selective access while maximizing space utilization up to 85%.
Send an Inquiry
Eliminate up to 80% of fixed aisles, double your usable pallet storage capacity, and cut cold room energy consumption by 40% with factory-direct solutions from CanalRack Industrial Storage S.A.
Maximum Storage Density & Direct Access
Combine 100% selective pallet accessibility with the footprint efficiency of dynamic motorized mobile bases.
Precision PLC & Safety Automation
Integrated photoelectric barriers, emergency stop sensors, and heavy-duty floor rails engineered for decades of maintenance-free operation.
ESTABLISHED 2004
At CanalRack Industrial Storage S.A., we specialize in solving the most complex space constraints faced by global procurement managers, logistics consultants, and cold chain operators. A Mobile Racking System (also known as Motorized Mobile Pallet Racking) represents the pinnacle of modern semi-automated high-density storage. By mounting heavy-duty rack superstructures onto electronically driven mobile chassis units that travel along precision-embedded floor rails, our systems consolidate multiple operating aisles into a single moving operational channel.
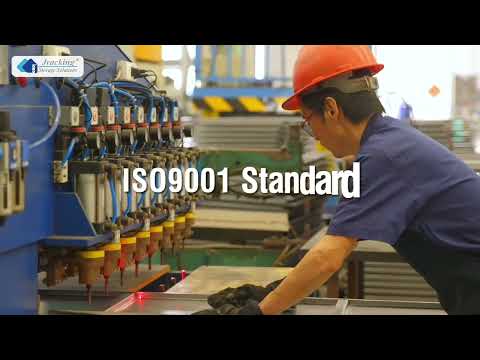
Operating from our 70,000 m² state-of-the-art intelligent manufacturing facility, CanalRack Industrial Storage S.A. processes over 100,000 tons of premium structural steel annually. Designed strictly according to international structural and safety frameworks—including European standards FEM 10.2.07 and EN 15095, American RMI guidelines, and ISO 9001 quality protocols—our mobile racking solutions deliver exceptional structural resilience, seismic safety, and operational longevity.
Comprehensive mechanical, electrical, and structural specifications designed for rigorous industrial demand and maximum ROI calculations.
| Technical Feature | Standard Specification | Heavy-Duty / Cold Storage Custom Option |
|---|---|---|
| Max Bay Load Capacity | Up to 24,000 kg (24 tons) per mobile carriage block | Custom engineered up to 36,000 kg for extra-heavy industrial dies & coils |
| System Height Range | 3,000 mm to 12,000 mm | High-bay customized options up to 15,000 mm with anti-tip guide rails |
| Travel Movement Speed | 4.0 to 5.5 meters per minute (Smooth acceleration/deceleration) | Frequency inverter-controlled variable speed (Soft-start / Soft-stop) |
| Operating Temperature | -5°C to +40°C Ambient Logistics Warehousing | -30°C to -40°C Deep Freeze Cold Storage (Heated cabinet panels & Arctic synthetic lube) |
| Control Architecture | Siemens / Schneider Microprocessor PLC with Touchscreen HMI | RF Remote Control, WMS/WCS Integration, Night-Park Energy Save Mode |
| Safety Compliance | EN 15095, FEM 10.2.07, SEMA, ISO 9001 | Seismic anchors, automated fire-sprinkler aisle parking synchronization |
| Rail Profile Integration | Precision Flat Rail / Dual Flange Guide Rail (C35 Concrete Flush) | Trackless surface-mounted guidance option for low-capacity retrofit sites |
With three specialized roll-forming and steel structural manufacturing bases, CanalRack Industrial Storage S.A. ensures rapid lead times, precise tolling, and stringent quality audits on every single component—from heavy cold-rolled upright columns to precision-machined steel wheels and PLC electrical panels.
CanalRack Industrial Storage S.A. engineers bespoke storage architectures engineered specifically for your building dimensions, pallet specs, ambient temperature, and SKU throughput speed.
Mounted on electric mobile bases with floor-guided rails. Provides 100% selective access while maximizing space utilization up to 85%.
Send an Inquiry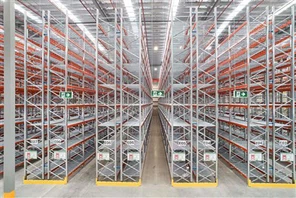
Specially treated low-temperature structural steel with moisture-sealed PLC boxes and thermal anti-freeze motor gearboxes.
Send an Inquiry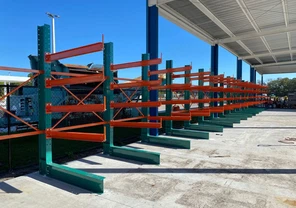
Eliminate aisles in long-item storage yards. Ideal for steel pipes, extrusions, plastic tubing, and timber packs.
Send an InquiryUltra-dense hybrid storage combining motorized mobile base movement with internal radio shuttle deep-lane pallet runners.
Send an Inquiry
2-inch pitch teardrop connection pattern built on heavy-duty motorized chassis for seamless integration with US supply chains.
Send an Inquiry
Enhances safety across mobile rack levels, allowing overhead light penetration and meeting strict fire sprinkler code compliance.
Send an Inquiry
High load capacity arms with boltless pitch adjustment, adaptable to both static and motorized mobile chassis bases.
Send an Inquiry
Engineered to AS 4084 structural safety standards for heavy mining, distribution, and manufacturing logistics operations.
Send an InquiryAs global supply chains navigate volatile warehouse real estate costs and escalating energy tariffs, industrial buyers are shifting rapidly from static storage layouts toward semi-automated motorized dynamic platforms. When evaluating a Mobile Racking System for upcoming capital expenditure (CapEx) investments, procurement leaders must account for several decisive market transformations:
The global industrial storage market is undergoing a structural transformation toward sustainable operational density. High-density storage is now directly aligned with corporate ESG (Environmental, Social, and Governance) targets. Constructing smaller warehouse footprints reduces concrete consumption, decreases land clearing, and lowers long-term building heating and cooling demands.
CanalRack Industrial Storage S.A. manufactures all racking components using eco-friendly, low-VOC electrostatic powder coatings and high-tensile structural steel profiles. By offering high dimensional accuracy and modular flexibility, our Mobile Racking System installations can be relocated, expanded, or reconfigured as your business model evolves, preventing premature infrastructure disposal and ensuring long-term asset protection.
Real-world engineering implementations across cold chain logistics, pharmaceutical fulfillment, automotive manufacturing, and chemical distribution centers.
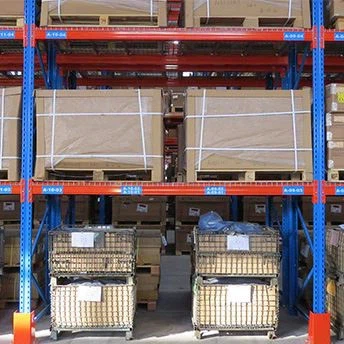
Replaced conventional selective pallet racking with CanalRack Mobile Racking, increasing pallet capacity from 4,200 to 7,800 positions inside a -25°C freezer hall without expanding the building shell.
Custom mobile bases carrying 24-ton rack loads enabled an automotive OEM to store heavy tooling dies directly adjacent to assembly lines, dramatically reducing internal travel times.
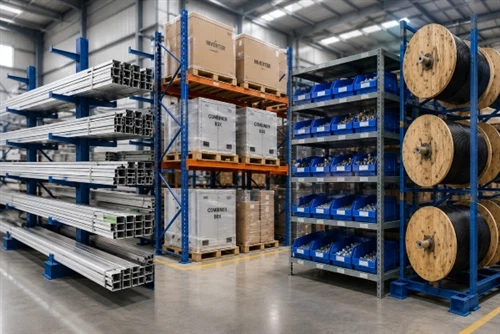
Integrated electric lockouts and RFID access tags on mobile carriage controls ensured compliance with strict regulated pharmaceutical storage and chain-of-custody tracking.
Equipped with specialized spill containment mesh and explosive-proof (ATEX-rated) motor drive options for chemical and coating product logistics.
From initial structural calculation to final electrical commissioning, we deliver end-to-end operational certainty.
In-depth technical and financial answers to key queries raised by engineering leads, procurement buyers, and warehouse operators evaluating motorized storage installations.
A conventional selective pallet rack system typically requires 60% of total warehouse floor area for forklift operating aisles, leaving only 40% for actual storage. A Mobile Racking System by CanalRack Industrial Storage S.A. eliminates all fixed aisles except one dynamic aisle. This increases usable storage density up to 80-85% within the exact same building footprint. For cold storage facilities where operational power costs are high, the reduction in required refrigerated volume yields a financial payback period (ROI) typically between 14 to 24 months.
Safety is the core foundation of CanalRack design. Our Mobile Racking Systems feature redundant safety barriers including: (1) Photoelectric light curtains running parallel across the length of every mobile carriage, stopping motion instantly if a person or forklift breaches an open aisle; (2) Mechanical pressure-sensitive bumper bars mounted at floor level; (3) Emergency stop pushbuttons on every control panel; and (4) Optical distance sensors preventing carriage collisions. All components are fully certified under EN 15095 (Power-operated movable racking).
Yes. CanalRack Industrial Storage S.A. specializes in deep-freeze mobile racking engineering. Low-temperature operations utilize specially treated fine-grain cold steel alloys that resist hydrogen embrittlement. Control panels contain internal IP65-rated heating elements to prevent condensation on PLC microprocessors, and drive gear motors are charged with synthetic low-viscosity Arctic lubricants designed for continuous operation down to -30°C.
Send an Inquiry for our Cold Storage Whitepaper.
Precision embedded rails must be anchored into C30/C35 structural concrete slabs meeting DIN 18202 Group 4 slab elevation tolerances. CanalRack Industrial Storage S.A. provides complete rail installation kits including leveling shims, chemical anchor bolts, and non-shrink epoxy grout specifications. We offer both "pre-cured slab channel embedding" for new construction and "shallow surface milling" options for retrofitting existing facilities.
In the event of a facility power failure, CanalRack Mobile Racking Systems can be coupled directly to an auxiliary backup diesel generator or UPS supply. Additionally, our heavy-duty drive gearboxes feature a manual clutch release mechanism, enabling maintenance technicians to disengage motor brakes and manually hand-crank or winch carriages to access critical pallets in an emergency.
Simply send your warehouse architectural floor plans (CAD or PDF), clear ceiling height, pallet dimensions (W x D x H), load weight per pallet, and operational temperature requirements to [email protected] or click below to submit an instant inquiry. Our senior engineering team will provide a comprehensive layout drawing, structural load report, and competitive factory-direct quote within 24 hours.
Partner with CanalRack Industrial Storage S.A. for custom-engineered Mobile Racking Systems delivered worldwide.